Getting a clean weld on 1/8-inch mild steel, roughly 11-gauge material, is less about one “magic” number and more about balancing voltage, wire feed speed, wire size, gas, and technique. When I dial in MIG welder settings for 1/8 steel, I start with the manufacturer’s chart and then run a test bead on scrap from the same material.
A common rule of thumb for 0.125-inch mild steel is about 125 amps, but joint type, position, wire diameter, gas, stick-out, and machine design can change the final setup.
What Settings Should I Start With for 1/8-Inch Mild Steel?
For clean indoor welding, a common setup is ER70S-6 solid wire with 75% argon and 25% CO2, or C25. With .030-inch wire, start around 17–18 volts. Some references use about 140–160 IPM, while other machine charts run substantially higher, which shows why your welder’s door chart should take priority. Following the correct settings also plays an important role in controlling risks from welding, including excessive spatter, poor fusion, overheating, and inconsistent bead quality.
With .035-inch solid wire, 18–19 volts and roughly 230–250 IPM are useful starting figures. Gas flow around 18–22 CFH for .030 wire and 20–22 CFH for .035 wire works well indoors. Maintaining proper gas coverage, electrical settings, and machine adjustments helps improve weld reliability while supporting safer working practices.
Your welder’s door chart or manual should always take priority because manufacturers design those recommendations around the machine’s actual output characteristics.
Is .030 or .035 MIG Wire Better for 1/8 Steel?
Both can handle 1/8-inch mild steel. I usually prefer .030 ER70S-6 for brackets, tubing, automotive repairs, and garage fabrication because it offers good heat control. Miller lists .030 wire for about 40–145 amps, covering the approximate 125-amp demand here.
A .035 wire is useful when the same machine regularly handles thicker steel because it carries more current comfortably and deposits filler faster.
What Shielding Gas and Polarity Should I Use?
C25 is a strong all-around choice for solid-wire MIG on mild steel. It gives a stable arc, relatively low spatter, and a smooth bead. Straight CO2 can provide deeper penetration but usually produces a harsher arc and more spatter.
With ER70S-6 solid wire, use DCEP, or direct-current electrode positive. If you switch to self-shielded flux-core, check the spool label before changing polarity. Many common self-shielded wires use DCEN, but the wire manufacturer’s instructions should decide the setup.
What Flux-Core Settings Work for 1/8-Inch Steel?
Flux-core is useful outdoors, on farms, around trailers, or anywhere wind can disturb shielding gas. For .030- or .035-inch self-shielded wire, a starting range around 19–21 volts and 200–220 IPM may work on some gasless machines.
Other charts may recommend lower numbers, so treat these only as baselines; wire chemistry, diameter, polarity, and machine output can change the correct values.
How Do I Fine-Tune Voltage and Wire Feed Speed?
A properly tuned short-circuit MIG arc should sound crisp and steady, often compared with frying bacon. I change one setting at a time.
If the wire stutters, pushes the gun backward, drives into the workpiece, or balls up before fusing, the wire feed may be too fast for the selected voltage. Reduce WFS slightly or raise voltage in a small step.
If the wire repeatedly burns back into the copper contact tip or the puddle becomes excessively wide and fluid, the voltage may be too high or WFS too low. Small corrections are usually better than large jumps.
What Gun Angle and Stick-Out Should I Use?
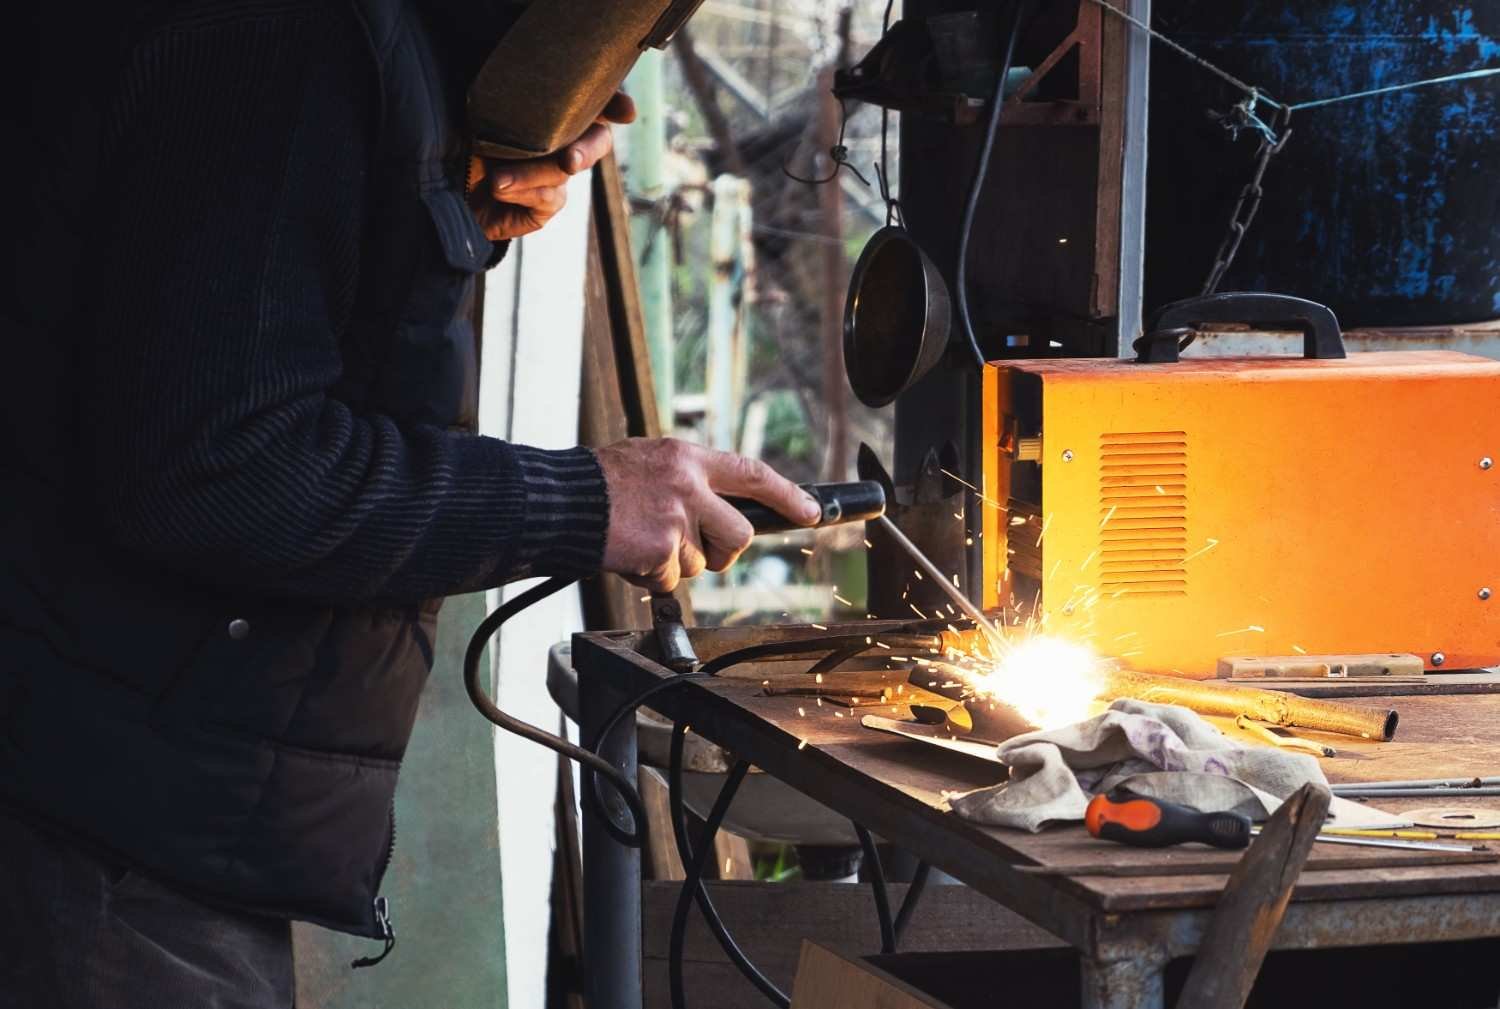
For flat welding with solid wire, I generally use a 10–15-degree push, or forehand, angle. This improves puddle visibility and usually gives a flatter bead with clean tie-in.
For .030 solid wire in short-circuit transfer, about 3/8 inch of stick-out is a practical starting point. Excessive or inconsistent stick-out can reduce effective heat and make a good machine setting feel unstable.
Do Butt, Lap, and T-Joints Need Different Settings?
Yes. A tight butt joint may need slightly less heat than a lap or T-joint because fillet welds have more surrounding metal absorbing heat and acting as metal as a heat shield during the welding process. Large gaps also increase burn-through risk because the arc has less material to support the weld pool and control heat distribution.
I clean paint, rust, grease, and heavy mill scale first because accurate settings cannot compensate for poor fit-up or contaminated steel. Proper surface preparation improves penetration, reduces defects, and helps maintain consistent weld quality.
How Can I Tell If My MIG Settings Are Too Hot or Too Cold?
Too much heat may cause undercut, a wide puddle, or burn-through. Reduce voltage slightly, travel faster, or rebalance wire speed.
A cold weld often looks tall or rope-like and fails to wet into the base metal. Poor toe fusion can mean the joint has not bonded properly.
When I fine-tune mig welder settings for 1/8 steel, I look for consistent bead width, smooth toe transition, controlled spatter, and proper fusion rather than relying only on the numbers shown on the machine.
Can a 120V MIG Welder Weld 1/8-Inch Steel?
Yes. Many 120V MIG welders sold in the US can weld 1/8-inch mild steel if the machine is rated for the thickness and connected to an appropriate circuit. A 240V machine normally offers more output headroom and a longer duty cycle, but 240V is not automatically required.
Always check the machine’s rated material capacity rather than judging welding capability from input voltage alone.
Frequently Asked Questions (FAQs)
1. What are the best mig welder settings for 1/8 steel?
With .030 ER70S-6 wire and C25 gas, start around 17–18 volts, then use your machine’s chart for wire feed speed. Roughly 18–22 CFH gas flow, DCEP polarity, and about 3/8-inch stick-out provide a useful baseline.
2. How Many Amps Do I Need for 1/8-Inch Mild Steel?
A common rule is about one amp for every .001 inch of steel thickness. Since 1/8 inch equals .125 inch, that suggests roughly 125 amps. Actual current depends heavily on wire diameter and wire feed speed.
3. Can I Use .035 Wire on 1/8-Inch Steel?
Yes. .035 solid wire works well, particularly when your welder also handles thicker material. .030 wire remains a versatile choice when easier heat control matters.
4. Should I Push or Pull the MIG Gun?
With solid wire and shielding gas, I normally use a 10–15-degree push angle for flat welding. For self-shielded flux-core, follow the wire manufacturer’s technique and polarity guidance.
Final Thoughts
I never assume one voltage-and-wire-speed combination will work perfectly on every machine. I start with the welder manufacturer’s chart, select the correct wire, gas, and polarity, and test on scrap. I also consider mig welder amp usage, because current draw and welding output can vary depending on the machine, material thickness, wire diameter, and settings.
Aim for a stable arc, smooth toe tie-in, controlled penetration, and manageable spatter. If you see undercut, burn-through, cold lap, or poor fusion, adjust in small steps. That approach is far more reliable than copying a single voltage and IPM combination without considering the welder, wire, joint, and working conditions.